
language
Exploring High Barrier Films in Packaging Design Services
Discover the significance of high barrier films in the realm of packaging design services and gain insights into their role in preserving product quality and extending shelf life. Learn about the scie
High Barrier Films: Preserving Quality and Enhancing Packaging Design
Introduction:
In the world of packaging design services, high barrier films play a crucial role in ensuring product quality and extending the shelf life of various goods. Let's delve into the realm of high barrier films and understand their significance in preserving the freshness and integrity of products.
1. Understanding High Barrier Films:
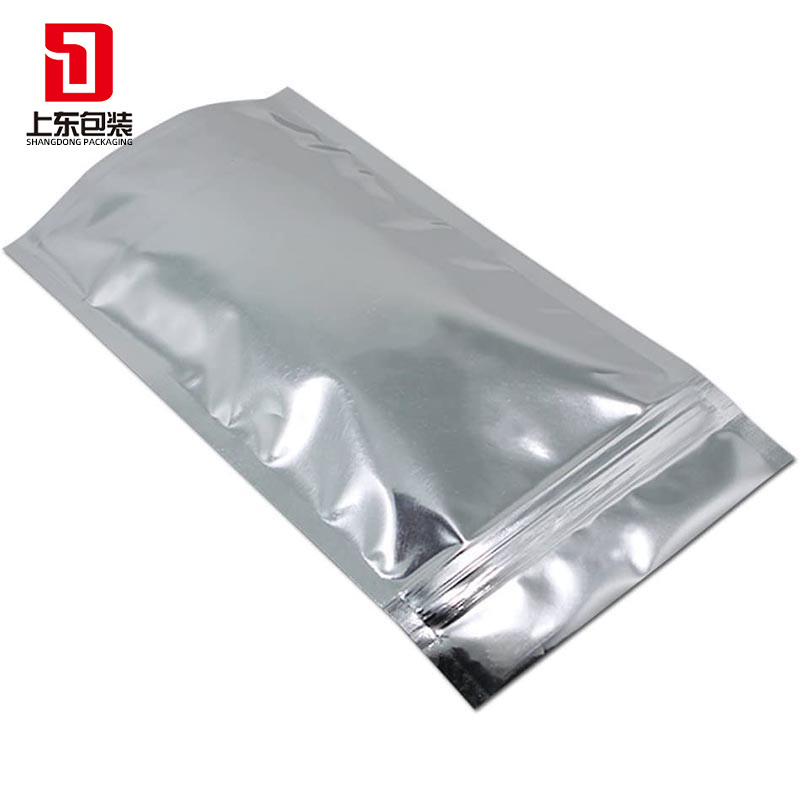
High barrier films are advanced packaging materials designed to prevent the permeation of gases, moisture, and light. Their primary purpose is to create a protective barrier that safeguards the product from external factors, such as oxygen, water vapor, and UV radiation.
2. Science behind High Barrier Films:
High barrier films are typically composed of multiple layers, each with specific properties. These layers could include materials such as polyethylene, polypropylene, polyester, and aluminum. The combination of these materials provides the film with exceptional barrier properties, ensuring minimal transmission of gases and moisture.
3. Applications in Packaging Design:
High barrier films find extensive use in various industries, including food, pharmaceuticals, electronics, and more. In the food industry, they are employed to package perishable items like meat, cheese, and baked goods, as well as to preserve the flavor and aroma of coffee and snacks. In the pharmaceutical industry, these films protect medications from moisture and oxygen, maintaining their efficacy.
4. Benefits of High Barrier Films:
By using high barrier films in packaging design, businesses can offer several advantages to their customers. These include:
a. Extended Shelf Life: High barrier films prevent spoilage and preserve product quality, resulting in an extended shelf life for goods.
b. Freshness and Taste Preservation: The films' exceptional barrier properties help retain the freshness, flavor, and aroma of food and beverages, enhancing the overall consumer experience.
c. Product Protection: High barrier films safeguard products from external factors such as moisture, gases, and UV radiation, ensuring they reach customers in optimal condition.
d. Sustainability: Some high barrier films are recyclable and eco-friendly, contributing to sustainable packaging practices.
Conclusion:
High barrier films are indispensable in the packaging design services industry, enabling the preservation of product quality and extending shelf life. By employing these advanced materials, businesses can ensure that their goods reach customers in optimal condition, offering enhanced freshness and protection. Understanding the science behind high barrier films empowers designers and businesses to make informed choices for their packaging needs, resulting in improved customer satisfaction and brand reputation.
Tag:
Recommend News

The Art of Crafting Eye-Catching Pet Food Packaging
The Art of Crafting Eye-Catching Pet Food Packaging
Introduction: The Importance of Pet Food Packaging
In the competitive landscape of pet food products, **packaging** plays a pivotal role in attracting customers. As pet owners increasingly seek quality and nutrition for their furry friends, the first impression often begins with the packaging. Effective pet food packaging not only protects the pr
Unleashing Creativity in Coffee Bag Packaging: Design Innovations for a Captivating Brand Experience
Unleashing Creativity in Coffee Bag Packaging
Table of Contents
Introduction to Coffee Bag Packaging
The Importance of Creative Design in Packaging
Types of Coffee Bag Packaging
Sustainable Packaging Solutions for Coffee
Material Selection for Coffee Bags
Branding and Marketing Through Packaging
Trends in Coffee Bag Design
Case Studies of Innovative Coffee Bag Pack
Exploring the Future Innovations for China Retort Pouches: A Comprehensive Guide
Exploring the Future Innovations for China Retort Pouches
Table of Contents
1. Introduction to Retort Pouches
2. The Importance of Retort Pouches in the Food Industry
3. Technological Advancements in Retort Pouch Production
4. Innovative Materials Used in Retort Pouches
5. Sustainability Trends in Retort Pouch Manufacturing
6. Diverse Applications of Retort Pouches
7.


Mobile:
WhatsApp:
E-mail:
Main Products
VR
Tiktok
GET A QUICK QUOTE
* Leave your contact information to get a free product quote